Maximizing perimeter storage efficiency within commercial and residential
developments centers on solving the dead corner dilemma. Kitchen and millwork
layouts inevitably encounter intersecting walls where standard linear cabinetry
fails to utilize volumetric space effectively. When evaluating corner cabinets
wholesale, contract specifiers, project developers, and architectural
procurement managers must look beyond surface aesthetics. Long-term commercial
success hinges on load-bearing structural integrity, dynamic kinematics, joinery
tolerances, and manufacturing repeatability across high-volume container
shipments.
Navigating the balance between square-foot spatial optimization and project
margins demands a comprehensive understanding of base, wall, and tall corner
configurations. Procurement decisions impact not only raw material budgets, but
also installation velocity on the jobsite and post-occupancy performance.
Selecting the correct corner unit architecture requires an analytical breakdown
of kinetic accessories, substrate performance, and modular production
capabilities.
Kinematic Geometries: Architectural Configurations of Corner Cabinetry
Corner base units dictate the dimensional flow of an entire architectural
kitchen layout. Any dimensional deviation at the corner amplifies down the
entire run, creating alignment issues for sink centers, integrated appliances,
and run terminations. Manufacturers classify corner storage into three primary
structural archetypes, each serving distinct floor plans and spatial
footprints.
Blind Corner Base Units
Blind corner cabinets extend past the intersecting cabinet run, hiding a
non-visible section behind a dead panel or adjoining drawer base. Standard
overall unit widths range from 36 inches (914 mm) to 48 inches (1219 mm),
requiring an opening reveal typically between 15 inches (381 mm) and 21 inches
(533 mm). The primary engineering challenge lies in accessing the blind recess
without compromising structural rigidity.
Clearance allowances: A systemic minimum clearance of 2 inches (50 mm) to 3
inches (76 mm) using filler strips prevents handle-to-handle interference with
adjacent perpendicular runs.
Load distribution: The horizontal floor rail requires continuous floor
contact or adjustable ABS leveling legs positioned directly beneath the blind
partition to prevent sagging under concentrated interior loads.
Flexibility: Non-handed universal configurations permit on-site adaptation,
allowing inventory consolidation for large-scale multi-family phases.
L-Shaped and Pie-Cut Corner Units
L-shaped corner cabinets follow the exact orthogonal footprint of the wall,
typically requiring a 36-inch by 36-inch (914 mm x 914 mm) footprint. These
units feature bi-fold doors linked by specialized 135-degree or 165-degree
hinges that collapse outward to expose the full interior volume without a
central dividing stile.
Bi-fold door stability: Heavy continuous daily cycling places significant
torque on the primary hinge mounting plates. Industrial specifiers require
minimum 1.5 mm cold-rolled steel mounting plates secured via Euro-screws
directly into core substrate pilot holes.
Structural overhead: Cantilevered interior corners require reinforced
diagonal top stretchers to preserve a precise 90-degree square angle during
transport, transit, and countertop installation.
Diagonal Base and Wall Corner Cabinets
Diagonal units cap the corner at a 45-degree angle to provide a continuous,
unbroken countertop transition or upper wall line. Standard diagonal wall
cabinets measure 24 inches by 24 inches (610 mm x 610 mm) with a diagonal front
door profile. While structurally rigid due to their triangular framing geometry,
diagonal units demand generous room clearances to avoid visual bulkiness in
compact urban apartment floor plans.
Kinetic Hardware Systems and Internal Mechanical Solutions
Volumetric space is functionally useless if the end-user cannot access it
effortlessly. Specifying modern hardware transforms otherwise dark, unreachable
voids into dynamic storage solutions. The hardware ecosystem selected for
commercial projects procuring corner cabinets wholesale directly dictates
end-user satisfaction and warranty claims over the life of the asset.
Articulated Pull-Out Trays (LeMans Style)
Articulated swinging trays move independently on controlled paths, extending
entirely outside the carcass perimeter. Controlled kinematic tracking paths
allow full shelf access with minimal door opening angles, typically around 85
degrees.
Dynamic load ratings: Commercial-grade articulated systems must withstand
minimum dynamic loads of 25 kg (55 lbs) per tray without vertical track
deflection exceeding 1.5 mm.
Bearing mechanisms: High-grade systems incorporate maintenance-free POM
(polyoxymethylene) polymer rollers paired with hardened steel guide tracks to
ensure silent sliding friction below 35 decibels.
Damper integration: Bi-directional soft-closing hydraulic or pneumatic
dampeners prevent bounce-back when users close fully loaded trays with
aggressive force.
Twin-Shelf Revolving Lazy Susan Assemblies
Revolving circular or kidney-shaped shelves remain the baseline specification
for multi-family developments where durability, simplicity, and low maintenance
take precedence over complex articulation. Rotational mechanisms anchor either
to an adjustable central aluminum/steel vertical axle or directly to fixed side
panels using cantilevered ball-bearing rings.
Axle-mounted configurations: Telescoping central columns constructed of
chrome-plated or powder-coated tubular steel (minimum wall thickness 1.2 mm)
adjust vertically between 26 and 32 inches to fit diverse carcass ceiling
heights.
Bearing construction: Heavy-duty steel ball bearings enclosed in
self-lubricating raceways provide smooth 360-degree continuous rotation.
Tray compositions: Rotomolded high-density polyethylene (HDPE) trays deliver
extreme impact resistance, while 12 mm solid plywood trays edged with
chrome-plated wire galleries cater to premium interior palettes. Essent Home
aligns internal hardware integrations with internationally rated cycle standards
to preserve kinematic smoothness under maximum domestic loads.
Full-Extension Blind Corner Pull-Outs (Magic Corners)
Rectangular pull-out mechanisms use an interdependent dual-frame linkage.
Opening the cabinet door pulls a front set of wire baskets forward while
simultaneously dragging the rear storage baskets from the blind recess into the
primary opening zone.
Slide mechanics: Heavy-duty synchronized under-mount slides handle
simultaneous front and lateral translation, demanding high lateral rigidity to
eliminate rack-and-pinion binding.
Total load thresholds: Multi-tier dynamic frame units support combined loads
up to 50 kg (front baskets 15 kg total, rear baskets 35 kg total).
Substrate Specifications and Structural Joinery Standards
Corner units bear immense dead loads. When granite, quartz, or sintered stone
countertops sit atop an interconnected run, corner carcasses often carry a
disproportionate amount of surface weight, especially where seam cutouts occur
nearby. The choice of core material and joinery technique defines whether a
cabinet maintains dimensional stability over decades or suffers joint
separation.
| Substrate Type | Standard Thickness | Density (kg/m³) | Internal Bond Strength | Primary Application Profile |
|---|
| Marine-Grade Birch Plywood | 18 mm (3/4 in) | 680 – 720 | ≥ 1.0 N/mm² | High-humidity zones, high-load countertops, ultra-premium
developments |
| High-Density Fiberboard (HDF) | 16 mm – 18 mm | 780 – 850 | ≥ 0.8 N/mm² | Precision CNC routing, profiled cabinet fronts, structural
stability |
| Moisture-Resistant Melamine Faced Chipboard (MR-MFC) | 18 mm (3/4 in) | 650 – 680 | ≥ 0.45 N/mm² | Commercial developments, cost-engineered hospitality
projects |
Joinery engineering requires deliberate consideration. Standard face-frame
designs depend on pocket-hole screws combined with PVA type II water-resistant
adhesives. Conversely, European frameless (full access) carcasses rely on
precision 8 mm fluted beechwood dowels paired with eccentric cam-and-pin
mechanical fasteners on 32 mm system drilling grids.
Advanced manufacturing facilities operated by Essent Home utilize automated
multi-axis CNC routers to achieve carcass panel dimensional tolerances within
±0.2 mm. This exactness eliminates squareness discrepancies that could cause
diagonal binds during rapid jobsite installation. Furthermore, edge sealing on
all exposed core edges uses zero-joint PUR (polyurethane) hot-melt adhesive or
hot-air laser edging technology. PUR adhesives provide unmatched structural
resistance to moisture vapor, steam, and ambient humidity, preventing localized
core swelling at structural corner seams.
Industrial Supply Chain Optimization: Flat-Pack (RTA) vs. Rigid
Pre-Assembled
Logistical efficiency dictates overall procurement economics when importing
large batches of corner units. Because corner base cabinets take up substantial
cubic space—a standard 36x36 inch base unit occupies roughly 0.75 cubic meters
(26.5 cubic feet) when fully assembled—freight costs quickly erode baseline
manufacturing savings if shipping configuration is miscalculated.
Ready-To-Assemble (RTA) Flat-Pack Strategy
Flat-pack packaging reduces shipping volume by 60% to 75% compared to
pre-assembled boxes, packing significantly more units into a 40-foot High Cube
(40HQ) container. For large projects with access to low-cost regional staging
facilities and skilled carpentry labor, flat-pack represents the most
cost-efficient procurement method.
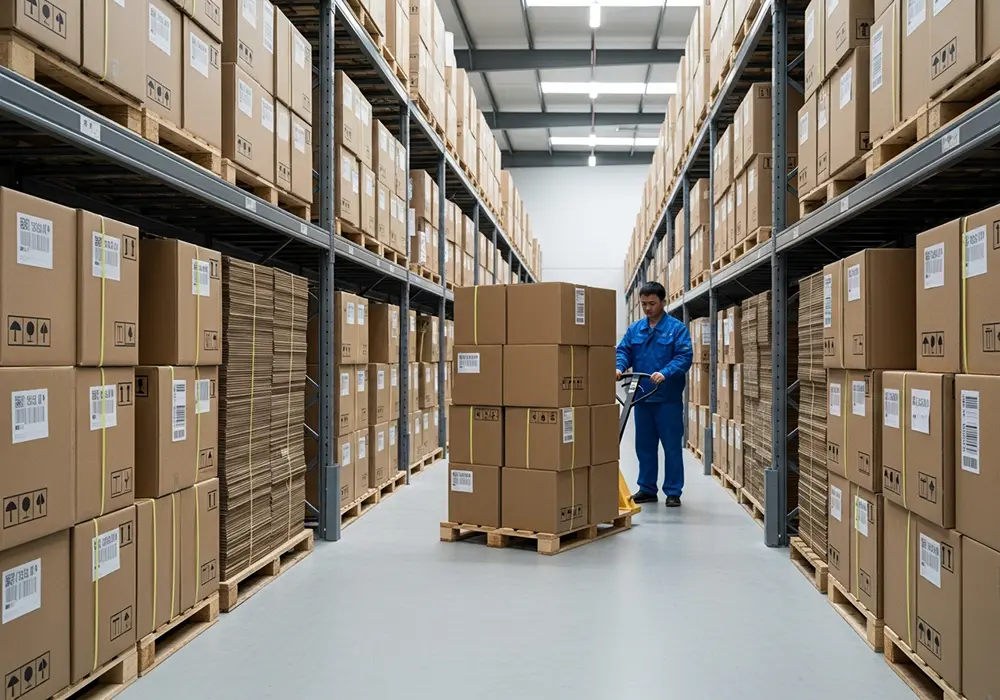
Packaging safeguards: Corner panels require 5-ply double-wall corrugated
cartons (bursting test grade ≥ 200 psi) with 20 mm high-density expanded
polystyrene (EPS) foam edge caps to protect fragile male/female dowels and
pre-milled grooves during oceanic shipping.
Hardware staging: Fasteners, shelf pins, and cam-locks are vacuum-sealed in
labeled blister packs matching specific assembly steps, reducing jobsite
hardware misplacement.
Rigid Factory Pre-Assembled Units
Pre-assembled cabinets arrive fully squared, doweled, glued, and clamped in
industrial pneumatic case clamps at the factory. This approach maximizes
consistency and minimizes installation hours on active construction sites.
Dimensional squareness: Automated pneumatic case clamps ensure panels dry
under uniform pressure, guaranteeing carcasses match precise 90-degree internal
tolerances.
Site labor reduction: Eliminating assembly stations on the construction
floor accelerates unit handover, making rigid assemblies advantageous where
trade labor wages are high.
Shipping protection: Rigid corner cabinets require internal corner
triangular bracing blocks and perimeter corrugated wrapping to endure the
multi-axis vibration typical of ocean transit.
The global logistics protocols maintained by Essent Home streamline
palletization, optimizing container stowage patterns to prevent hollow voids and
maximize gross container tonnage without exceeding maritime weight
limitations.
Quality Control, Testing Protocols, and Environmental Standards
Procuring corner cabinets wholesale requires stringent adherence to
international building codes, material emissions regulations, and hardware
endurance benchmarks. Sourcing teams must audit production lines for process
controls that prevent field degradation.
Mechanical Durability Testing
Dynamic hardware mechanisms must undergo accelerated lifecycle testing
certified by independent inspection bodies. Testing benchmarks based on
ANSI/BHMA A156.9 (Grade 1) and European EN 14749 standards evaluate cabinet
carcass and component resilience:
Cycle durability: Articulated blind corner trays and revolving systems
undergo 50,000 to 100,000 continuous open-and-close cycles under maximum design
loads to verify zero mechanical failure or hinge sagging.
Static shelf loading: Shelving components must support 1.5 times the rated
load for continuous periods of 7 days without permanent structural deflection
exceeding L/150 of the span.
Salt spray exposure: All metal brackets, chrome wire baskets, and slides
undergo neutral salt spray testing (ASTM B117) for a minimum of 96 hours without
exhibiting visible red oxidation or surface pitting.
Emissions and Environmental Certification
Substrates used in multi-tenant or commercial architectural projects must
comply with regional environmental and public safety statutes. Panel goods must
carry verifiable mill test certificates to ensure compliance:
CARB Phase 2 / EPA TSCA Title VI: Formaldehyde emission limits set below
0.05 ppm for plywood and particleboard substrates.
FSC (Forest Stewardship Council) Chain of Custody: Ensuring timber
substrates trace directly back to responsibly managed forests.
RoHS Compliance: Verifying electroplated dynamic components, coatings, and
plastic liners contain zero hazardous heavy metals such as lead, mercury, or
hexavalent chromium.
Procurement Strategy: Aligning Specification with Project Margins
Mastering bulk procurement involves evaluating corner cabinets wholesale
catalogs against architectural blueprints long before issuing requests for
proposal (RFPs). Successful commercial millwork contracts utilize value
engineering to balance tactile user touchpoints with concealed structural cost
optimizations.
Working alongside Essent Home provides architects and commercial developers
direct access to bespoke manufacturing configurations. This approach allows
teams to align project tiers seamlessly:
Multi-family urban towers: Utilize moisture-resistant MFC carcasses with
dowel-and-cam joinery, paired with smooth-operating, post-mounted twin Lazy
Susan turntables. This strategy delivers rugged durability and low maintenance
costs across hundreds of identical rental units.
Luxury condominiums: Shift specifications to 18 mm birch multi-ply
carcasses, zero-joint PUR edge banding, soft-close articulated LeMans-style
internal tracking units, and continuous lacquer fronts with custom wood veneer
grain-matching.
Hospitality and boutique commercial spaces: Implement custom diagonal or
non-standard angle geometries driven by 5-axis CNC routing, featuring heavy-duty
drawer box slide extensions rated for high-frequency use.
Integrating these technical specifications directly into standard bid
documentation guarantees uniform factory quoting, preventing cost revisions or
material compromises during bulk production runs.
Frequently Asked Questions (FAQ)
What is the minimum clearance needed for blind corner cabinet door
hardware?
Standard architectural guidelines require a minimum clearance filler of 2
inches (50 mm) to 3 inches (76 mm) between the blind corner cabinet front and
the adjacent perpendicular cabinet run. This clearance allows door pulls,
handles, and adjacent appliance doors to cycle fully open without colliding or
marring adjacent finishes.
Does Essent Home provide full certification for low-formaldehyde building
requirements?
Every commercial production run produced by Essent Home can be specified and
certified in full compliance with CARB Phase 2, EPA TSCA Title VI, and European
E1/E0 emission standards. Independent testing documentation and material
chain-of-custody certificates accompany shipment manifests for seamless
regulatory inspection.
How does packaging differ between flat-pack (RTA) and pre-assembled corner
cabinets?
Flat-pack corner units pack dense, flat-panel components into heavy-duty
5-ply cartons lined with protective foam edge guards and moisture barrier film,
maximizing container space. Rigid pre-assembled units are packed in individual
wooden crates or corner-protected corrugated wrap with internal structural
gussets to hold the 90-degree square angle stable throughout multi-modal
transport.
Which internal corner mechanism offers the greatest weight capacity for
commercial applications?
Heavy-duty, axle-supported rotating Lazy Susan assemblies with center steel
posts provide the highest structural weight distribution, supporting up to 30 kg
per shelf. For blind corners, heavy-duty dual-slide rectangular pull-out frames
handle total loads up to 50 kg across their front and rear basket arrays.
Can corner base cabinets accommodate under-mount corner sinks?
Diagonal corner base cabinets (minimum 36x36 inches or 42x42 inches) can
accommodate under-mount corner sinks, provided front structural apron rails are
appropriately engineered. In contrast, standard 90-degree L-shaped or blind
corner cabinets rarely support under-mount sinks due to intersecting carcass
partitions and structural countertop seam locations.
What is the standard lead time for high-volume wholesale cabinet production
runs?
Standard factory manufacturing cycles for multi-container production range
from 30 to 45 business days following shop drawing sign-off and material
specification approval. Total project timelines must also account for ocean
freight transit times, which vary depending on destination ports and logistical
corridors.
Initiating Technical Specifications and Custom Bulk Quotations
Large-scale commercial developments demand reliable precision, tight
dimensional tolerances, and uncompromised supply chain stability. Transitioning
from conceptual designs to physical container delivery requires seasoned
manufacturing oversight, production scalability, and rigorous quality controls
at every stage of the joinery and assembly process.
Submit your architectural schedule, material schedules, and hardware
specifications to partner with Essent Home to finalize dimensional drawings,
structural bill of materials, and production milestones for your upcoming
procurement phases.